 Welding of thermoplastic parts热塑性塑料件的焊接
|

|
1. Cut the crack into a V-shaped section and prepare for welding1. 将裂纹切成V型断面,准备进行焊接
1 Use a scraper to cut a V-shaped weld with an opening angle of 60~70°.用刮刀切割成V型焊缝,焊缝开口角度为60~ 70°。
2 Use a 3mm drill bit to drill holes at the ends of the cracks to prevent them from extending. If the edge of the weld is uneven, use clamps to repair the beginning of the crack before starting welding, and then drill holes at the end of the crack.在裂缝的末端用3mm的钻头钻孔以防裂缝延伸。如焊缝边缘不平,开始焊接前先用夹钳修理裂缝开始部位,然后在裂缝末端钻孔。
|
|
2. Set the welding temperature (200~700℃) according to the manufacturer's specified value, and the thickness of the plastic material and welding rod determines the welding temperature2. 根据制造商规定值设置焊接温度(200~700℃),且塑料材料和焊条的厚度决定焊接温度
1 Preheat the welding equipment for 3~4 minutes to reach the pre-selected welding temperature.对焊接设备进行3~4min的预热,使其达到预先选定的焊接温度。
2 Cut the front end of the welding rod into a bevel so that it gradually fills in from the beginning of the crack weld.将焊条的前端切成斜面,以便从裂缝焊缝的开始位置起逐步填充。
|
 |
|
3. Welding3. 焊接
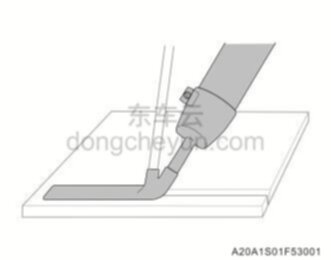
1 Push the welding rod with the beveled front end into the heated rapid welding nozzle preheating chamber until the tip of the welding rod is exposed from the lower part. When the welding rod and the parts to be welded are in a plastic state, the welding operation can be started. When performing plastic welding, stable welding speed and stable operating pressure are required. Only apply pressure to the electrode when welding.将前端切成斜面的焊条推入已加热的快速焊接喷嘴预热腔,直到焊条的尖端从下部露出。当焊条和待焊接部位件处于塑性状态时,可开始焊接操作。进行塑料焊接时要有稳定的焊接速度和稳定的操作压力。焊接时仅对焊条施加压力。
2 The lower end of the quick welding nozzle must move parallel to the repair surface. Parallel movements over larger lengths are achieved by appropriate tilting of the welding equipment.快速焊接喷嘴的下端必须和修理表面平行移动。在较大长度方向上的平行移动是通过焊接设备的合适倾斜来实现。
|
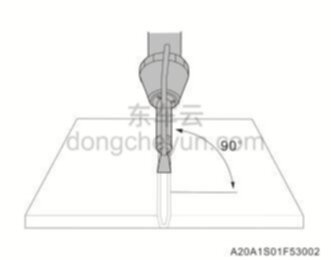 |
3 When moving the plastic welding gun, keep the electrode perpendicular to the weld seam.移动塑料焊枪时,保持焊条与焊缝垂直。
|
 |
4. Check welded joints4. 检查焊接接头
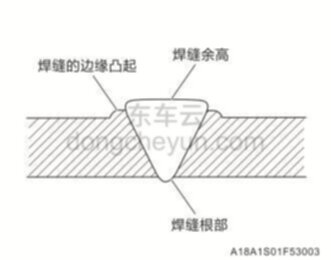
1 If only a small or smooth bulge is formed along the edge of the weld during welding, it indicates that the welding effect is ideal. This is very critical for bevel welding. Check the weld from the back for the following defects and re-weld if necessary:如焊接时沿焊缝边缘只形成了很小的或平滑的凸起,则表明焊接效果理想。这对开坡口的焊缝焊接非常关键。从背部检查焊缝是否有下列缺陷,并在必要时重新焊接:
|
|
5. Rework welds5. 重新加工焊缝
1 After cooling, the raised portion of the weld can be ground with an angle grinder.在冷却后,焊缝的凸起部分可用角度砂轮机进行打磨。
2 The surface is then sanded with an orbital grinder.然后用轨道砂轮机进行表面打磨。
3 Use a plastic cleaning brush to clean the repair surface.使用塑料清洁刷清洁修理表面。
4 Spray plastic primer over the repair surface.在修理表面上喷涂塑料底漆。
|